How to Select a Sonic Soot Blower: Frequency, Coverage and Installation Requirements
Selecting a sonic soot blower requires more than comparing frequency and acoustic output. Deposit characteristics, equipment geometry, installation distance, compressed-air supply and structural resonance all influence the effectiveness of acoustic cleaning. This guide explains the main engineering selection factors and introduces the SHEENWAY Sonic Soot Blower product range.
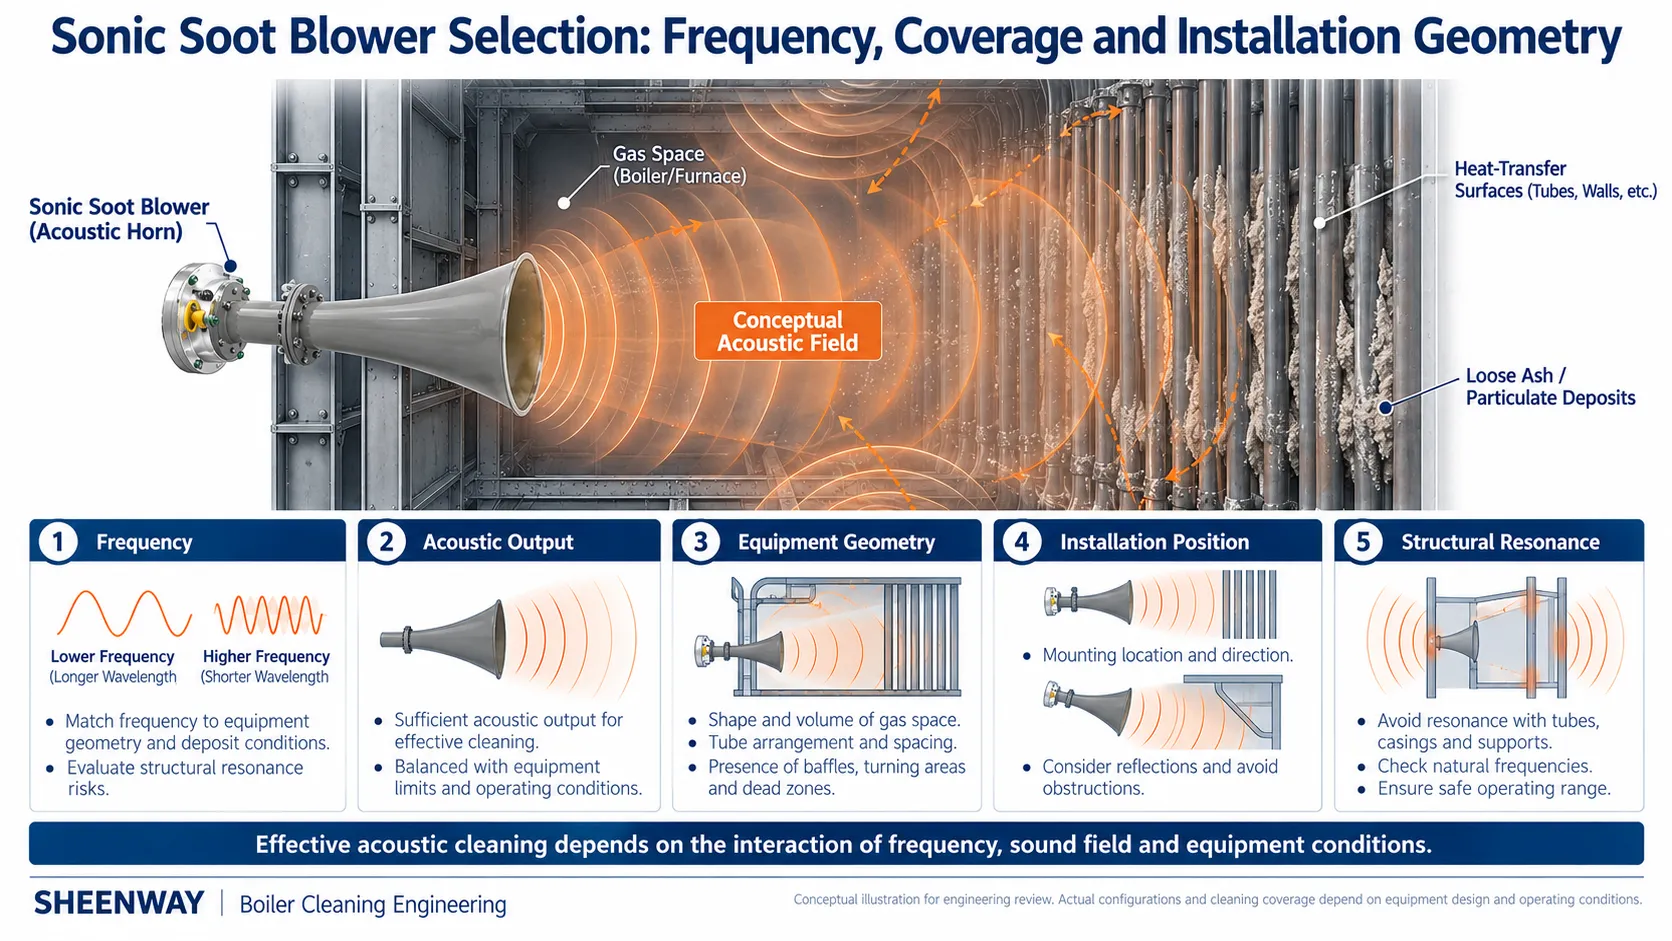
A sonic soot blower uses acoustic energy rather than a concentrated steam jet to help remove deposits from industrial equipment.
This makes it a useful cleaning option for certain boiler sections, dust-collection systems, heat exchangers and material-handling equipment.
However, selecting a Sonic Soot Blower is not simply a matter of choosing the lowest available frequency or the highest advertised acoustic output.
Two acoustic cleaners with different frequencies may perform differently in the same vessel. Even the same model may produce different cleaning results when installed in equipment with different internal dimensions, obstructions and deposit characteristics.
The engineering challenge is therefore to determine whether an appropriate sound field can be established in the target cleaning area.
For this reason, sonic soot blower selection should consider several factors together:
Deposit characteristics, operating frequency, acoustic output, equipment geometry, installation position and structural safety.
This guide explains the main selection principles and introduces the relevant features of the SHEENWAY Sonic Soot Blower range.
1. Understanding the Working Principle of Acoustic Cleaning
A conventional steam soot blower directs a high-velocity jet toward deposits on a heating surface.
A Sonic Soot Blower operates through a different mechanism.
In a typical compressed-air-driven acoustic cleaner, compressed air powers a sound generator. The generated pressure pulses are transmitted through an acoustic horn into the surrounding gas space.
These periodic pressure fluctuations can cause deposited particles to experience relative movement, vibration and changes in adhesion.
Under suitable conditions, loosely attached material can become detached from the surface.
Once loosened, particles may fall under gravity or be carried away by the process gas stream.
The important distinction is that acoustic cleaning does not primarily depend on a nozzle delivering concentrated high-velocity steam directly to each target surface.
Instead, the cleaning action is associated with acoustic pressure fluctuations propagating through the equipment.
This can be useful in equipment containing relatively complex internal structures, where direct access by a cleaning jet may be limited.
However, acoustic propagation through a vessel does not guarantee effective cleaning at every location.
The sound field depends on the equipment geometry, acoustic source and installation arrangement.
2. The First Selection Question: What Type of Deposit Is Present?
Before selecting a frequency, the deposit itself should be evaluated.
Acoustic cleaning is generally most relevant for deposits that can be loosened through repeated pressure fluctuations.
These may include relatively loose fly ash, dust and certain particulate accumulations.
According to EPRI's technical literature on ash deposits and deposit removal, sonic horns can be effective for loose ash and very lightly sintered deposits.
However, their ability to remove strongly bonded or hard deposits is limited.
This distinction is important.
A dry particulate deposit may respond to acoustic cleaning.
A sticky deposit formed through condensation or chemical reactions may behave differently.
Dense slag, strongly sintered deposits or material that has fused to a heating surface may require another cleaning mechanism.
Therefore, the first selection question should not be:
“Which frequency is the most powerful?”
It should be:
“Can this deposit reasonably be loosened by acoustic pressure fluctuations?”
If the answer is uncertain, the deposit condition should be investigated before selecting equipment.
3. Why Frequency Matters
Frequency describes the number of pressure oscillations occurring each second.
It is measured in hertz (Hz).
For example, a nominal frequency of 75 Hz represents 75 oscillation cycles per second.
Frequency affects acoustic wavelength and influences the interaction between sound waves, equipment geometry and deposited particles.
In general, lower-frequency sound often experiences less attenuation during propagation through industrial gas spaces and may be useful for applications requiring broader acoustic influence.
However, this does not establish a universal relationship between lower frequency and better cleaning.
The actual acoustic field also depends on:
- sound-source characteristics;
- acoustic output;
- gas conditions;
- equipment dimensions;
- internal structures;
- and the position of the acoustic source.
A lower-frequency unit is therefore not automatically suitable for every large vessel.
Likewise, a higher-frequency unit is not automatically unsuitable for industrial cleaning.
Frequency is one part of the acoustic design, not a complete measure of cleaning performance.
4. Lower Frequency Does Not Always Mean Better Cleaning
A common selection mistake is to assume that the lowest available frequency provides the greatest cleaning performance.
This assumption ignores the relationship between the acoustic source and the surrounding structure.
Every industrial vessel has its own geometry and mechanical characteristics.
Certain components may possess natural vibration frequencies.
If an acoustic source produces sufficient excitation near a relevant structural resonance, undesirable vibration can occur.
Research published in the journal Acoustics has discussed the importance of controlling acoustic energy input in industrial boiler-cleaning applications to address vibration and noise-related concerns.
SHEENWAY's product documentation likewise identifies structural natural frequencies as an important consideration when selecting acoustic-cleaning frequencies.
Therefore, frequency selection should include an assessment of the equipment's structural response.
This does not mean that every low-frequency sonic soot blower will cause damaging resonance.
It means that frequency suitability must be established for the actual installation rather than assumed from the nominal frequency alone.
5. Acoustic Output Is Not the Same as Effective Cleaning Coverage
Another important product parameter is the Acoustic Output Level.
SHEENWAY's published Sonic Soot Blower specifications include nominal acoustic output levels of 145 dB, 147 dB and 150 dB across different models.
These values characterize the acoustic output of the respective products under their specified reference conditions.
However, they should not be interpreted as direct measurements of cleaning performance at every point inside a boiler or dust collector.
The acoustic pressure reaching a particular surface can be influenced by:
- distance from the sound source;
- acoustic attenuation;
- reflection and interference;
- internal obstructions;
- equipment geometry;
- and operating gas conditions.
For this reason, a model with a nominal output of 150 dB cannot automatically be considered more effective than a 145 dB model in every application.
Furthermore, acoustic output ratings should not be confused with occupational noise exposure measurements.
Personnel noise exposure must be assessed using appropriate measurement methods at relevant workplace locations.
The correct engineering objective is to establish sufficient acoustic action in the required cleaning region while respecting equipment and personnel safety requirements.
6. Equipment Geometry Determines How Sound Propagates
A Sonic Soot Blower does not operate in an empty laboratory chamber.
Real industrial equipment may contain tube bundles, structural supports, catalyst modules, collecting plates, ducts or hoppers.
These structures influence sound propagation.
The dimensions of the enclosure, the presence of internal partitions and the available gas passages can all affect the acoustic field.
For example, a large open chamber and a tightly packed tube bank may respond differently to the same acoustic source.
Similarly, a long duct with several bends presents a different propagation environment from a relatively compact dust-collection hopper.
This is why installation geometry must be considered together with frequency and acoustic output.
A useful equipment review should identify:
Overall dimensions
The size and shape of the target enclosure.
Internal structures
Tube banks, plates, support beams and other obstacles.
Required cleaning locations
Where deposits accumulate and which surfaces require acoustic action.
Available mounting positions
Where the sound generator and acoustic horn can be installed.
Operating conditions
Temperature, gas composition and any special environmental restrictions.
These details help determine whether the proposed acoustic-cleaning arrangement is suitable.
7. Installation Position Can Be as Important as Frequency
Even when a suitable Sonic Soot Blower model has been selected, installation position can influence the result.
The acoustic horn should be arranged to transmit energy into the intended cleaning space.
Potential installation points may include suitable existing openings, access locations or dedicated mounting interfaces.
However, the presence of an opening does not automatically make it an appropriate acoustic-cleaner location.
The selected position should be evaluated for:
- transmission into the target gas space;
- obstructions near the outlet;
- equipment-wall integrity;
- local temperature;
- maintenance access;
- and the surrounding structural arrangement.
For large equipment, multiple acoustic cleaners may be considered if one installation cannot provide the required coverage.
The number and position of the units should follow a project-specific review.
Acoustic-cleaner quantity should not be determined solely from equipment volume without considering geometry and the required cleaning locations.
8. Structural Resonance and Personnel Noise Must Be Evaluated
Acoustic cleaning deliberately introduces pressure fluctuations into industrial equipment.
While these fluctuations can help loosen deposits, the equipment structure and surrounding workplace must also be considered.
Structural vibration assessment may be appropriate where the selected acoustic frequency could interact with sensitive equipment components.
Potential concerns include local vibration of panels, supports or other structural elements.
The purpose of the assessment is to avoid undesirable structural responses while providing suitable acoustic-cleaning action.
Personnel noise is another separate consideration.
The U.S. Occupational Safety and Health Administration (OSHA) explains that workplace noise exposure depends on the sound pressure experienced by workers and the duration of exposure.
Therefore, the nominal acoustic output of a Sonic Soot Blower should not be treated as the measured workplace noise level.
Where necessary, installation design may require appropriate acoustic isolation, operating controls, access restrictions or other protective measures.
These requirements should be evaluated according to the applicable site and regulatory conditions.
9. Compressed-Air Supply Is Part of the Selection
SHEENWAY Sonic Soot Blowers use compressed air to power the acoustic sound generator.
This means that the available air supply must be reviewed before selecting a model.
Important parameters include:
Available pressure
The supply must satisfy the selected generator's operating requirements.
Air consumption
The compressor and distribution system must provide the required flow during operation.
Air quality
The air supply must meet the equipment's requirements for moisture, contamination and other relevant conditions.
Operating sequence
The selected cleaning cycle and control arrangement must be compatible with the plant.
Supply-system capacity
Where multiple units operate, the air system must support the intended operating sequence.
A nominally suitable sonic soot blower may not achieve its specified operating condition if the compressed-air supply is insufficient.
Therefore, the acoustic source and air-supply system should be considered together.
10. Understanding the SHEENWAY Sonic Soot Blower Range
SHEENWAY offers Sonic Soot Blowers with different nominal frequencies, acoustic output ratings, materials and physical configurations.
The current product range includes several frequency and construction families.
| SHEENWAY Model | Fundamental Frequency | Acoustic Output Level | Product Characteristics |
|---|---|---|---|
| SW-ALLH | 75 Hz | 147 dB | Long-horn, heavy-duty configuration |
| SW-ALLS | 75 Hz | 147 dB | Long-horn, standard-duty configuration |
| SW-ALRS | 75 Hz | 147 dB | Radiused configuration |
| SW-AMCS | 230 Hz | 150 dB | Compact, standard-duty configuration |
| SW-AHCS | 360 Hz | 150 dB | Compact, standard-duty configuration |
| SW-AMFS | 220 Hz | 150 dB | Fluidizer-type configuration |
| SW-ALEL | 125 Hz | 145 dB | Enclosed, light-duty configuration |
| SW-AUEM | 25 Hz | 145 dB | Enclosed, medium-duty configuration |
| SW-AUEH | 25 Hz | 145 dB | Enclosed, heavy-duty configuration |
The descriptions reflect the company's official model classification.
They do not imply that one frequency or configuration is universally superior.
For example, two models with the same nominal fundamental frequency may differ in overall dimensions, materials, construction or installation requirements.
Conversely, a more compact unit with a different frequency should not automatically be considered an equivalent replacement.
Final selection must consider the actual application and the complete product specification.
A Note on Frequency Classification
SHEENWAY uses an internal model-code classification to organize the acoustic product range.
Within this system:
- Ultra-low Frequency: 50 Hz and below
- Low Frequency: 51–150 Hz
- Medium Frequency: 151–300 Hz
- High Frequency: Above 300 Hz
These bands are SHEENWAY's internal product classifications, not universal industry-standard frequency definitions.
The market-facing product name remains Sonic Soot Blower.
The cleaning technology may be described as acoustic cleaning or an acoustic cleaning system.
11. Where Are Sonic Soot Blowers Commonly Considered?
According to SHEENWAY's product documentation, potential applications include:
Boiler Tube Banks
For suitable particulate deposits where acoustic cleaning can provide useful preventative or supplementary action.
Electrostatic Precipitators
To support removal of dust deposits from collecting surfaces under appropriate operating conditions.
Baghouse and Dust-Collection Equipment
Where particulate accumulation or material flow problems may benefit from acoustic cleaning.
Hoppers and Material-Handling Equipment
To help reduce suitable dry material accumulation and support material movement.
Ducts and Heat Exchangers
Where the equipment geometry and deposit properties are compatible with acoustic cleaning.
SCR Reactors
In selected applications where acoustic cleaning is compatible with the catalyst arrangement and operating requirements.
Babcock & Wilcox notes that acoustic devices have been used for some SCR catalyst-cleaning applications where site-specific conditions allow.
This does not mean that acoustic cleaning is appropriate for every SCR installation.
The catalyst geometry, deposit characteristics and acceptable mechanical response must be evaluated.
12. When Is a Sonic Soot Blower Not the Right Solution?
A Sonic Soot Blower should not be selected simply because it provides non-contact cleaning.
There are applications where another cleaning method may be more suitable.
Examples include:
Strongly bonded slag
Acoustic pressure fluctuations may not provide sufficient removal action.
Sticky or wet deposits
The deposit may not respond effectively to acoustic loosening.
Severe chemical scaling
A different cleaning mechanism may be required.
Unfavorable acoustic geometry
The target region may not receive sufficient acoustic energy.
Unacceptable vibration or noise conditions
The installation may require a different frequency, arrangement or cleaning technology.
In these cases, a steam soot blower, water-cleaning system or another engineered cleaning method may be more appropriate.
Acoustic cleaning can also be used as a complementary method in suitable installations rather than replacing every existing soot blower.
13. What Information Should Be Provided Before Selection?
A useful Sonic Soot Blower inquiry should begin with the actual process equipment and deposit conditions.
| Information Required | Engineering Purpose |
|---|---|
| Equipment type and application | Defines the intended cleaning environment |
| Internal dimensions | Supports acoustic-coverage evaluation |
| Internal structure | Identifies obstructions and propagation conditions |
| Deposit characteristics | Determines whether acoustic cleaning is suitable |
| Deposit locations | Defines target cleaning areas |
| Operating temperature | Supports material and installation review |
| Existing cleaning arrangement | Identifies current limitations |
| Available mounting openings | Supports installation planning |
| Compressed-air pressure and capacity | Confirms utility compatibility |
| Structural and vibration considerations | Supports resonance-risk review |
| Noise and access requirements | Supports workplace safety evaluation |
| Desired cleaning operation | Defines scheduling and control requirements |
For retrofit projects, existing drawings and inspection photographs can help establish these conditions.
The supplier should not be expected to select an acoustic cleaner reliably from equipment dimensions alone.
14. How Should Acoustic Cleaning Performance Be Evaluated?
After installation, the acoustic cleaner should be evaluated according to the actual cleaning objective.
Depending on the application, useful observations may include:
- deposit accumulation trends;
- pressure-drop behavior under comparable operating conditions;
- material-flow performance;
- inspection findings;
- maintenance frequency;
- and any unexpected vibration or noise.
These indicators must be interpreted carefully.
For example, a reduction in pressure drop may reflect changes in process flow as well as changes in deposit accumulation.
Likewise, the absence of visible buildup near one installation point does not prove that all internal surfaces receive sufficient acoustic cleaning.
The objective is to determine whether the system controls the intended deposits under the actual operating conditions.
Conclusion
Sonic Soot Blower selection is fundamentally an acoustic-engineering problem.
Frequency is important, but frequency alone cannot determine whether a cleaning system will be effective.
Acoustic output, equipment geometry, installation position, deposit characteristics and compressed-air conditions all influence the resulting cleaning action.
Structural resonance and personnel noise must also be considered.
SHEENWAY offers Sonic Soot Blowers with different frequency ratings and mechanical configurations to accommodate different application requirements.
However, no individual frequency or model should be assumed suitable for every industrial cleaning problem.
The correct selection begins with the deposit and the equipment—not with the lowest frequency or highest acoustic output rating.
For new installations and retrofit projects, SHEENWAY can review the equipment geometry, operating conditions and deposit characteristics to assess an appropriate Sonic Soot Blower configuration.
More from Sheenway
Continue Reading
Retractable Boiler Temperature Probe: Why It Matters During Boiler Startup
During boiler startup, furnace exit gas temperatures can rise before sufficient steam cooling is established in certain heating surfaces. A retractable boiler temperature probe positions a thermocouple in the gas path to provide temperature information for operating decisions. This guide explains the working principle, startup applications, measurement limitations and selection requirements of the SHEENWAY SW-MTPS.
Read articleRake-Type Soot Blower Design for SCR: Nozzle Layout, Travel and Support
Rake-type soot blowers use non-rotating, axially moving cleaning assemblies to direct steam or compressed air toward SCR catalysts and other structured surfaces. This guide explains nozzle layout, travel, support and guide arrangements, cleaning-medium conditions and the engineering checks required before selecting or replacing a rake-type soot blower.
Read articleMulti-Medium Retractable Soot Blowers: When Steam Alone Is Not Enough
Steam soot blowing is effective for many boiler cleaning applications, but certain gypsum, salt and strongly bonded deposits may require additional cleaning methods. This guide explains how multi-medium retractable soot blowers combine different cleaning options, when water washing may be considered, and how engineers select an appropriate solution for gas-gas heaters and air preheaters.
Read article